Minimum order quantity
300 kg
The quotation confirms how the 300 kg minimum applies to the profile, tooling, finish and production route.
Technical capabilities
Explore Omalco's extrusion routes, materials, secondary operations and quality support for standard and custom aluminium profiles.
Capability index
Explore the profile, material, operation and quality capabilities relevant to an aluminium extrusion enquiry.
Planning markers
Use these planning markers as a starting point. The final schedule follows drawing approval, tooling, finish and order requirements.
Minimum order quantity
300 kg
The quotation confirms how the 300 kg minimum applies to the profile, tooling, finish and production route.
Typical lead time
21 days
The 21-day figure is a typical planning reference. The committed schedule follows drawing approval, tooling, finish and order requirements.
Capability 01
Press and profile limits used to establish whether a cross-section fits the available production route.
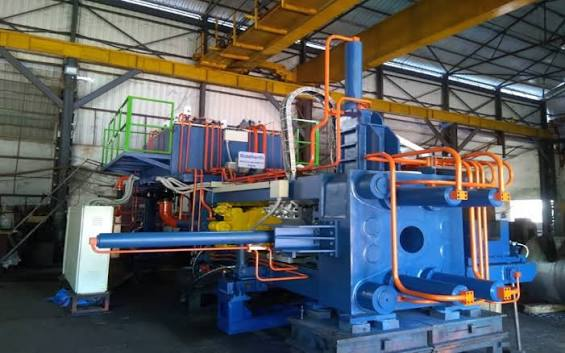
Extrusion presses
1,400 T and 750 T
The 1,400 T and 750 T press routes are reviewed against the cross-section, alloy and tooling requirement.
Billet diameters
6 in (152.4 mm) and 5 in (127 mm)
Company-provided billet sizes for the two available press routes.
Maximum profile CCD
160 mm larger press; 127 mm smaller press
Maximum circumscribing-circle figures supplied by Omalco; final fit still depends on geometry, alloy and tooling review.
Solid / hollow / semi-hollow
Drawing review required
Section classification and feasibility are confirmed during die and manufacturability review.
Capability 02
Alloy and temper selection starts with geometry, loading, finish, fabrication and service conditions.
Alloy routes
5000, 6000 and 7000 series
Omalco works across all 5000, 6000 and 7000 series aluminium alloys; final alloy and temper selection remains profile and application dependent.
Alloy selection support
Available during technical review
Buyers may submit an enquiry without knowing the alloy or temper.
Capability 03
Dimensional inspection is organized around the approved drawing and acceptance criteria.
Wall-thickness control
Drawing review required
Critical walls and functional interfaces should be identified on the submitted drawing.
Capability 04
Downstream work is reviewed with the extrusion so datums, allowances and handling remain coordinated.
Secondary operations
Cutting, drilling, tapping and machining coordination
The exact in-house and partner scope must be confirmed for each enquiry.
Surface finishing
Mill, anodized and powder-coated routes listed
Finish availability, specification and approved colour remain enquiry dependent.
Capability 05
Quality equipment supports alloy verification, mechanical testing and non-destructive inspection for agreed profile requirements.
Quality controls
Dimensional, surface, spectrometer and UTS checks
Spectrometer and UTS-machine availability is company provided; sampling plans and document scope remain order dependent.
Spectrochemical analysis
Spectrometer available
Company-provided equipment capability; method, calibration status and testing frequency are confirmed through the applicable quality plan.
Tensile testing
UTS machine available
Company-provided equipment capability; test method, specimen route and report scope are confirmed for the applicable requirement.
Ultrasonic inspection
Ultrasonic detector available
Company-provided equipment capability; instrument model, applicable flaw-detection method, calibration blocks and acceptance criteria require quality-plan confirmation.
Industrial X-ray inspection
X-ray detector available
Company-provided equipment capability; system type, approved inspection scope, radiation controls, method and reporting require controlled documentary confirmation.
Capability 06
Packing is planned around surface protection, handling, identification and delivery conditions.
Protective packing
Customer and destination dependent
Packaging material and protection are selected against customer handling needs and the delivery destination.
Bundling and labelling
Requirement dependent
Bundle weight, labels and handling instructions should be agreed before dispatch.
Export packing
Destination dependent
Packing is reviewed for the delivery route; any named export or packing standard must be agreed in the order.
Custom packaging
Available to customer requirement
Share surface sensitivity, handling route and delivery conditions so the material and pack format can be agreed.
Custom development
The gates remain consistent even when tooling, sampling, finish, secondary work or inspection requirements change.
Share a PDF, CAD file, image or controlled reference.
Review function, geometry, alloy, temper, finish and downstream operations.
Define the tooling route after manufacturability review.
Develop tooling against the approved section and review inputs.
Produce a trial route where new tooling or profile validation is required.
Inspect the sample against the agreed drawing and acceptance plan.
Record the approved revision before repeat production.
Run the agreed extrusion, finish and secondary-operation route.
Protect, identify and release profiles against the order requirement.
What to send
Unknown fields are acceptable. The application, critical geometry and expected production need matter more than a perfectly completed specification.
Technical resourcesBuyer questions
Use these answers to prepare your enquiry. The approved drawing and quotation define the requirements for your order.
Omalco's stated minimum order quantity is 300 kg. The quotation confirms how this applies to the profile, tooling, alloy, finish and production route. Send the required quantity for each profile for review.
Omalco lists a typical lead time of 21 days. This is a planning reference. The committed delivery schedule depends on drawing approval, new tooling, trials, finish, quantity and order requirements. Confirm the schedule in the quotation.
Yes. The technical team can review drawings, samples, target applications, finish requirements, and fabrication constraints before recommending the next development step.
Cutting, drilling, tapping, machining and finishing can be discussed with the extrusion enquiry. The quotation must identify the agreed operations and confirm which work is performed in house or through a coordinated partner. Share the finished-part drawing and acceptance requirements.
Share the profile drawing or reference, alloy and temper, finish, dimensions, estimated quantity, delivery location, target timeline, and application details.
Drawing-led RFQ
Send us your cross-section for manufacturability review. Alloy, temper and tolerance fields can be left unknown.